In Stock
Brand:
Cronatron™
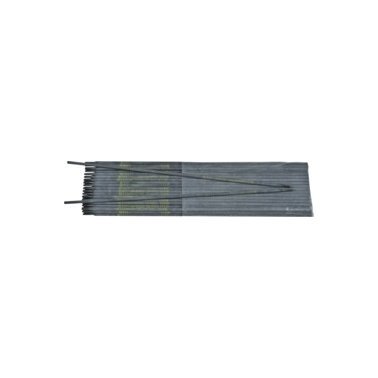
Cronatron™ 235 Cast Iron Stick Rod Electrode
Cronatron™ - 235 Cast Iron Stick Rod Electrode 1/8 " (5 US Pounds)

Welcome! Register now to see your pricing!
Close


Cronatron™ - 235 Cast Iron Stick Rod Electrode 1/8 " (5 US Pounds)
All-position welding for any type of weldable cast iron repair and cast iron to steel.
Superior Advantages
• High strength welds
• Fully machinable
• Pass-over-pass welding to save time
• All-position welding may eliminate the need to dismantle equipment to perform repairs
Iron-adding
Tensile Strength: 60,000 PSI
Polarity: AC or DC Reverse
235 is specifically formulated for welding on burned, rusty, corroded or otherwise contaminated cast iron parts not requiring machining.
Typical Applications
• Pump and bearing housings
• Cylinder blocks and heads
• Machine bases
• Manifolds and exhaust systems
Usage Procedure:
Remove grease, scale and other impurities from weld area. Bevel cracks or breaks (70° to 90° “V”). CRONACUT™ 1100 is the fastest and easiest method to prepare section for weld repairing. Use a short to medium arc at the lowest possible amperage for best results. Employ weaving technique or stringer beads. Peen to relieve stress. Remove slag between passes. Slow cooling to room temperature recommended.

† May Require Additional Delivery Time to Canada

