In Stock
Brand:
Cronatron™
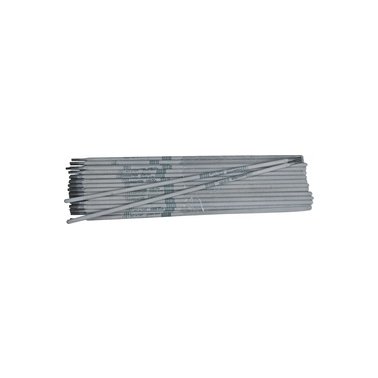
Cronatron™ 3000 Nickel Stick Rod Electrode
Cronatron™ - 3000 Nickel Stick Rod Electrode 5/32" (5 US Pounds)

Welcome! Register now to see your pricing!
Close


Cronatron™ - 3000 Nickel Stick Rod Electrode 5/32" (5 US Pounds)
Compatible with Inconel, other nickel-based alloys, Monel® and dissimilar alloys.
Superior Advantages
• Extremely corrosion-resistant
• High temperature usage – up to 2,000°F (1,093°C)
• Low temperature usage – down to –320°F (–196°C)
• Maximum versatility
• Dissimilar metals joining
Withstands operating temperatures from –320°F to +2,000°F (–196°C to +1,093°C).
Tensile Strength: 100,000 PSI
Elongation: 33%
Polarity: DC Reverse
Typical Applications
• Furnaces and boilers
• Heat treat baskets
• Power plants
• Chemical processing
Usage Procedure
Use DC reverse polarity with normal maintenance welding procedures. Surface should be as clean as possible. Hold a short arc and tilt electrode 10° in the direction of travel. Remove slag between passes. Preheating the weld metal is not necessary unless the base metal and/or thickness require it. Do not weave more than twice the diameter of the core wire.

† May Require Additional Delivery Time to Canada

