In Stock
Brand:
Cronatron™
Cronatron™ 45 Silver Bare Brazing Rod
Cronatron™ - 45 Silver Bare Brazing Rod 1/8 " (1 US Pound)


Welcome! Register now to see your pricing!
Close


Cronatron™ - 45 Silver Bare Brazing Rod 1/8 " (1 US Pound)
These “sil-phos” alloys provide cost-effective solutions to joining copper and brass alloys.
Superior Advantages
• Thin flow provides excellent capillary action
• No flux required for copper-to-copper applications
• Fills gaps on poor fit-up joints
Resists vibration, shock, impact
Brazing Range: 1,300°F to 1,450°F (704°C to 788°C)
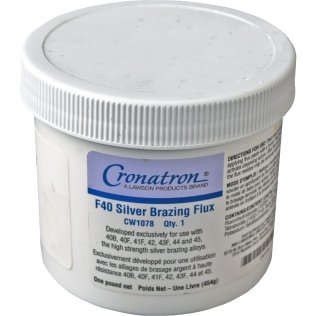
Recommended Flux: F40 (for dissimilar)
Typical Applications
• Electrical components
• Plumbing and HVAC
• Copper coils and tubing
• Rotors and armatures
Usage Procedure
Heat broad area using large torch tip; a neutral flame is suggested, and a distance of 2" to 3" from the base metal produces the best results. No flux is required on copper-to-copper welds. The joint area should be clean. When the copper turns dull red, the alloy should be applied and the flame should be kept in constant motion ahead of the rod. These alloys are especially effective on long lap joints, fillets and butts.

This product will be available later

† May Require Additional Delivery Time to Canada